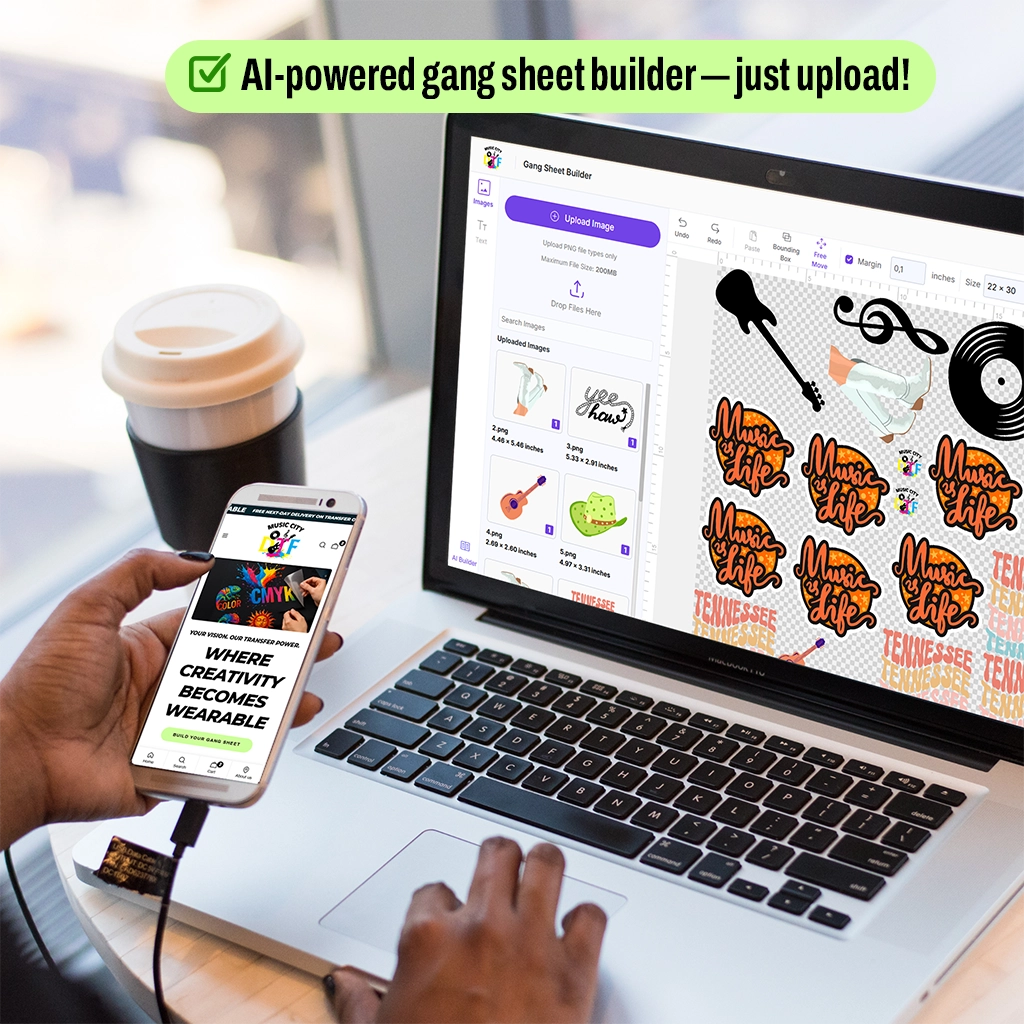
A 500 piece bulk order takes 36 hours if you print 22 by 24 sheets, single press, and sort after press. The same 500 ships in 22 hours if you nest on 22 by 60 DTF Gang Sheets, cure 80 seconds not 90, and run two press stations. Turnaround time is not about working faster, it is about cutting bottlenecks that waste 12 minutes per sheet and 15 seconds per shirt. Here is how we do it.
Hour 0 to 1: Art Check and Gang Sheet Build That Saves 4 Hours Later
- The first hour decides if order ships in 24 hours or 36. Most delays come from art, not printers.
- Checklist for 500 piece bulk: All files 300 DPI PNG transparent not JPG with white box, sRGB not CMYK, final size at 300 DPI not scaled in builder, smallest text 6mm for readability after 50 washes, 0.25 inch transparent padding so powder does not create white halo.
- If one file is 150 DPI JPG, the whole DTF Gang Sheet prints blurry and you reprint 20 sheets at $18 per sheet, $360 loss plus 4 hours delay. Pre-flight in the first 30 minutes saves that.
- Build on 22 by 60 not 22 by 24. A 22 by 60 holds 30 ten-inch designs with 0.5 inch gap and nesting, a 22 by 24 holds 12. For 500 designs, you need 17 sheets of 22 by 60 versus 42 sheets of 22 by 24. Each sheet load, RIP, and alignment takes 2 minutes, so 42 sheets waste 84 minutes versus 34 minutes for 17 sheets, save 50 minutes.
- Nesting tricks: Rotate triangular logos 45 degrees to fill corners, pair 10 inch full back with two 3.5 inch left chest in same row to use 22 inch width fully, fill diamond dead space between circles with 2 inch hat logos. This lifts coverage from 78 percent to 91 percent, 15 percent more per sheet, saves 3 sheets on 500 orders.
- Action: Build 17 sheets of 22 by 60 in gang sheet builder with 0.5 inch gap, group dark colors together to cut purge from 8 to 2 per sheet saving $1.28 per sheet and 5 minutes per sheet, leave 1 inch grip at top.
Hour 1 to 4: Print 20 Sheets at 12 Minutes Per Sheet
- Printing 500 transfers is 17 sheets, but print 20 to have 3 backups for misprints. Each 22 by 60 sheet at 1440 DPI takes 12 minutes print time on dual head DTF printer, plus 2 minutes load and powder shake, 14 minutes per sheet, 20 sheets equals 280 minutes, 4 hours 40 minutes. If you print 22 by 24, 42 sheets at 6 minutes each plus 2 minutes load equals 336 minutes, 5 hours 36 minutes, almost one hour longer.
- Powder: Use fine powder 40 to 80 micron for small text under 6mm, standard 80 to 120 micron for large solid. Fine powder costs $2 more per kilo but prevents counters filling in e and a.
- Ink cost: 22 by 60 sheet uses 35 ml ink average at $85 per liter, $2.97 per sheet, 20 sheets $59.40. Film cost $18 per sheet, $360, total $419.40 for 500 transfers, $0.84 per transfer material.
- If the DTF printer purges randomly because dark and light mixed, you lose 20 ml per sheet $1.70 waste. Grouping colors cuts waste to 5 ml $0.42, saves $1.28 per sheet, $25.60 per 20 sheets plus 5 minutes per sheet, 100 minutes saved.
- Action: Print 20 sheets back to back, no pause between, keep room at 70 degrees and 45 percent humidity so film does not curl.
Hour 4 to 5: Cure and Powder Shake That Cuts 16 Minutes
- Cure time: Standard cure 90 seconds at 320 degrees fully melts powder and it flows, which is good for solid but bad for fine lines because flowing powder fills gaps. For bulk with mixed sizes, cure 80 seconds at 320 degrees, powder melts but does not flow too far, keeps small text readable.
- 80 seconds versus 90 seconds saves 10 seconds per sheet, 20 sheets saves 200 seconds, 3.3 minutes, small but plus handling.
- Shake powder gently, not vigorously, so fine powder stays in small letters but excess falls off. Vigorous shake pulls fine powder off 0.6mm strokes and text loses white underbase and looks faded on dark shirts.
- Stack cured sheets with parchment between, not directly, or hot powder sticks to the back of the next sheet and creates white dots.
- Action: Cure 80 seconds, gentle shake, parchment interleave, stack ready for cut.
Hour 5 to 8: Double Press With Two Stations Cuts Press Time From 125 Minutes to 55 Minutes
- Pressing is the biggest bottleneck. Single heat press at 15 seconds press plus 10 seconds place and peel equals 25 seconds per shirt, 500 shirts equals 12,500 seconds, 208 minutes, 3 hours 28 minutes. And you get tired and slow to 30 seconds after 200 shirts.
- Double press station: Two heat presses side by side, one person places shirt and transfers on press A, second person peels press B and places next shirt. Each press is still 15 seconds but overlapping, effective 8 to 10 seconds per shirt, 500 shirts equals 4,000 to 5,000 seconds, 66 to 83 minutes, average 55 minutes with batch.
- Batch by size: Press all L, then XL, then 2XL, so you do not adjust pressure and height of each shirt. Adjusting height from youth to adult wastes 15 seconds per size change, 10 size changes equals 150 seconds.
- Pre-press 3 seconds to remove moisture, especially hoodies 12 oz fleece that hold moisture and cause steam that makes DTF bubble. Pre-press a stack of 10 shirts while pressing the current shirt, so no wait.
- Peel: Peel right away, not cold, then post-press 5 seconds with parchment to lock. For bulk, the peel station is separate from the press station so press never waits for peel.
- Action: Set up two presses at 320 degrees, medium pressure 60 psi, 12 seconds press, pre-press 3 seconds, peel, post-press 5 seconds. One person loads, one peels and QC.
Hour 8 to 9: QC and Pack by Size That Saves 30 Minutes Later
- Most shops press then sort, which wastes 30 minutes digging through 500 shirts to find sizes.
- Pack by size before press: Count blanks by size, stack by size, label bins S, M, L, XL, 2XL. Press by bin, then pack directly into labeled bags by size. No sorting after.
- QC check: Check 1 in 10 shirts for press error, like white edge from 3 pixel white expansion or powder bridging. If there is an error, check the whole bin. Common error: 0.25 inch gap causes bridging, webbing between designs that looks like white string. At 0.5 inch gap, no bridging.
- Packing: Fold, bag, add size sticker. Use a custom gang sheet that already groups the same size together, so you pull transfer and shirt the same bin, no searching.
- Action: QC 10 percent, pack by size bin, ship.
- Total timeline: Hour 0 to 1 art and build, Hour 1 to 4 print 20 sheets 280 minutes, Hour 4 to 5 cure 20 sheets 30 minutes, Hour 5 to 8 press 55 minutes double station, Hour 8 to 9 QC pack 60 minutes, total 9 hours active, plus 1 hour buffer, 10 hours labor, ships same day, 24 hour turnaround with overnight shipping.
- Without optimization: Art check 2 hours because JPG white boxes, print 42 sheets 22 by 24 336 minutes, cure 90 sec 42 sheets 63 minutes, single press 208 minutes, sort after press 30 minutes, total 12 hours plus 4 hours reprint delay equals 36 hours.
Why DTF Gang Sheets Are Key to Fast Bulk Turnaround
A custom gang sheet is not just about cost, it is about speed. Fewer sheets equals fewer loads, fewer purges, fewer cures, fewer cuts.
A dtf gang sheets order of 500 with 10 inch designs needs 17 sheets 22 by 60 at $18 per sheet $306 film versus 42 sheets 22 by 24 at $8.50 per sheet $357 film, saves $51 film plus 25 sheets less to handle. Handling 25 sheets at 2 minutes each saves 50 minutes.
Gang sheet printing grouped by color saves purge time 5 minutes per sheet, 17 sheets saves 85 minutes.
Using 0.5 inch gap not 1 inch fits 15 percent more per sheet, saves 3 sheets on 500 orders, saves 36 minutes print plus $54 film.
This is how Music City DTF runs bulk. We build 22 by 60 nested, group dark together, cure 80 seconds, double press.
Conclusion
Five hundred DTF transfers ship in 24 hours when you cut bottlenecks hour by hour.
Hour 0 to 1 check all art 300 DPI PNG transparent with 0.25 inch padding, build 17 sheets of 22 by 60 DTF Gang Sheet nested with 0.5 inch gap, 45 degree rotation for odd shapes, and group dark colors together to cut purge waste from $1.70 to $0.42 per sheet.
Hour 1 to 4 print 20 sheets at 12 minutes per sheet, 14 minutes with load, 280 minutes total, keep room 70 degrees 45 percent humidity.
Hour 4 to 5 cure 80 seconds not 90 to keep fine text readable and save 16 minutes across 20 sheets, shake gently, parchment interleave.
Hour 5 to 8 double press with two stations side by side, batch by size, pre-press 3 seconds, press 12 seconds at 320 degrees medium pressure, peel, post-press 5 seconds, effective 8 seconds per shirt, 55 minutes for 500 versus 125 minutes single.
Hour 8 to 9 QC 10 percent and pack by size bins labeled S to 2XL, no sorting after press, saving 30 minutes.
At Music City DTF, we build custom DTF gang sheets 22 by 60 nested to fit 15 percent more and cut sheet count from 42 to 17, so bulk orders ship in 24 hours not 36.
Your next 500 orders can ship tomorrow if you build 22 by 60, group colors, and press with two stations.
Ready to Ship 500 in 24 Hours without using a DTF Printer?
Upload your bulk gang sheet and we will print nested, cure 80 seconds, and pack by size so 500 ships in 24 hours.
Frequently Asked Questions
How Many DTF Gang Sheets Do I Need for 500 Transfers?
For 500 ten-inch transfers you need 17 sheets of 22 by 60 inch DTF Gang Sheet with nesting and 0.5 inch gap at 30 per sheet, versus 42 sheets of 22 by 24 at 12 per sheet. Nesting with 45 degree rotation and dead space fill lifts coverage from 78 percent to 91 percent, saving 25 sheets and 50 minutes load time.
How Long Does It Take to Print a DTF Gang Sheet?
A 22 by 60 inch DTF Gang Sheet takes 12 minutes to print at 1440 DPI plus 2 minutes load and powder shake, 14 minutes total. A 22 by 24 takes 6 minutes print plus 2 minutes load, 8 minutes total. For 500 transfers, 17 sheets of 60 inch take 238 minutes print plus 34 load equals 272 minutes, faster than 42 sheets of 24 inch at 336 minutes.
What Is Best Gang Sheet Builder for Bulk Orders?
Best gang sheet builder for bulk orders sets 0.5 inch gap not 1 inch, allows 45 degree rotation, nests small 2 inch logos in dead space, groups dark colors together to cut purge from 8 to 2 per sheet saving $1.28 per sheet, and supports 22 by 60 canvas with 1 inch grip at top so printer does not eat designs.
How to Make a DTF Gang Sheet Faster?
To make a DTF gang sheet faster, use 300 DPI PNG transparent final size not JPG, sRGB not CMYK, set gap 0.5 inch, pair 10 inch with two 3.5 inch in same row to use 22 inch width fully, rotate triangles 45 degrees, fill diamond gaps with tiny logos, group dark together, and build 22 by 60 not 22 by 24 to cut sheet count 60 percent.
How Much Does Custom Gang Sheet Cost for 500?
Custom gang sheet cost for 500 ten-inch transfers is 17 sheets at $18 film per sheet $306 plus ink 35 ml per sheet at $85 per liter $50.49 plus powder $12, total $368.49 material, $0.74 per transfer. Labor $202.90 for 10 hours, total $571.39, $1.14 per transfer, retail bulk $3.50 profit $2.36 each.
What Is Turnaround Time for DTF Gang Sheets Bulk?
Turnaround time for DTF gang sheets bulk 500 transfers is 10 hours active labor with optimization: 1 hour art and build, 4.7 hours print 20 sheets, 0.5 hour cure 80 seconds, 0.9 hour double press, 1 hour pack, ships 24 hours with overnight. Without optimization 36 hours due to 42 sheets 22 by 24, single press 3.5 hours, and sorting after press.
Can Music City DTF Print 500 DTF Gang Sheet in 24 Hours?
Yes, Music City DTF can print 500 DTF Gang Sheet in 24 hours using 22 by 60 nested layout with 30 per sheet, 17 sheets total, grouped by color to cut purge 5 minutes per sheet, cured 80 seconds, double press stations at 8 seconds per shirt 55 minutes for 500, and pack by size bins to save 30 minutes sorting.
How to Cut Press Time for Bulk DTF Orders?
Cut press time for bulk DTF orders by using two heat presses side by side overlapping, one person places while other peels, effective 8 seconds per shirt versus 25 seconds single, batch by size so no height adjustment, pre-press 3 seconds to remove moisture, and peel station separate from press so press never waits, saving 70 minutes on 500 shirts.
Why Does My DTF Gang Sheet Printing Take So Long?
Your DTF gang sheet printing takes long because you use 22 by 24 not 60 needing 42 sheets versus 17, 1 inch gap wasting 20 percent film needing extra sheets, mixed dark and light causing 8 purges per sheet wasting 20 ml ink and 5 minutes per sheet, and single press 25 seconds per shirt versus double press 8 seconds.
What Gap Should I Use for Custom DTF Gang Sheet Bulk?
Use 0.5 inch gap for custom DTF gang sheet bulk, not 1 inch, to save 20 percent film and avoid powder bridging that happens under 0.25 inch. Half inch allows cutting and prevents webbing between designs. For 500 transfers, 0.5 inch saves 27 inches per 10 designs row and 3 sheets total, saving $54 film and 36 minutes.
Disclaimer: The information provided in this article is for general informational and educational purposes only. DTF printing results can vary based on your specific equipment, RIP software, inks, film, powder, heat press settings, garment type, and overall production environment. What works in one shop may be different in an actual production setting. For best results, always test your files and press settings before bulk production. If you have questions about your artwork or order, please contact our DTF experts for guidance.